AVR (Vikram) Valves is one of India’s largest engine valves manufacturers, serving global OEMs and the aftermarket since 1975.
Manufactured at our IATF 16949-certified facility in India, Vikram engine valves are engineered for durability, precise fitment, and consistent performance across global engine platforms.
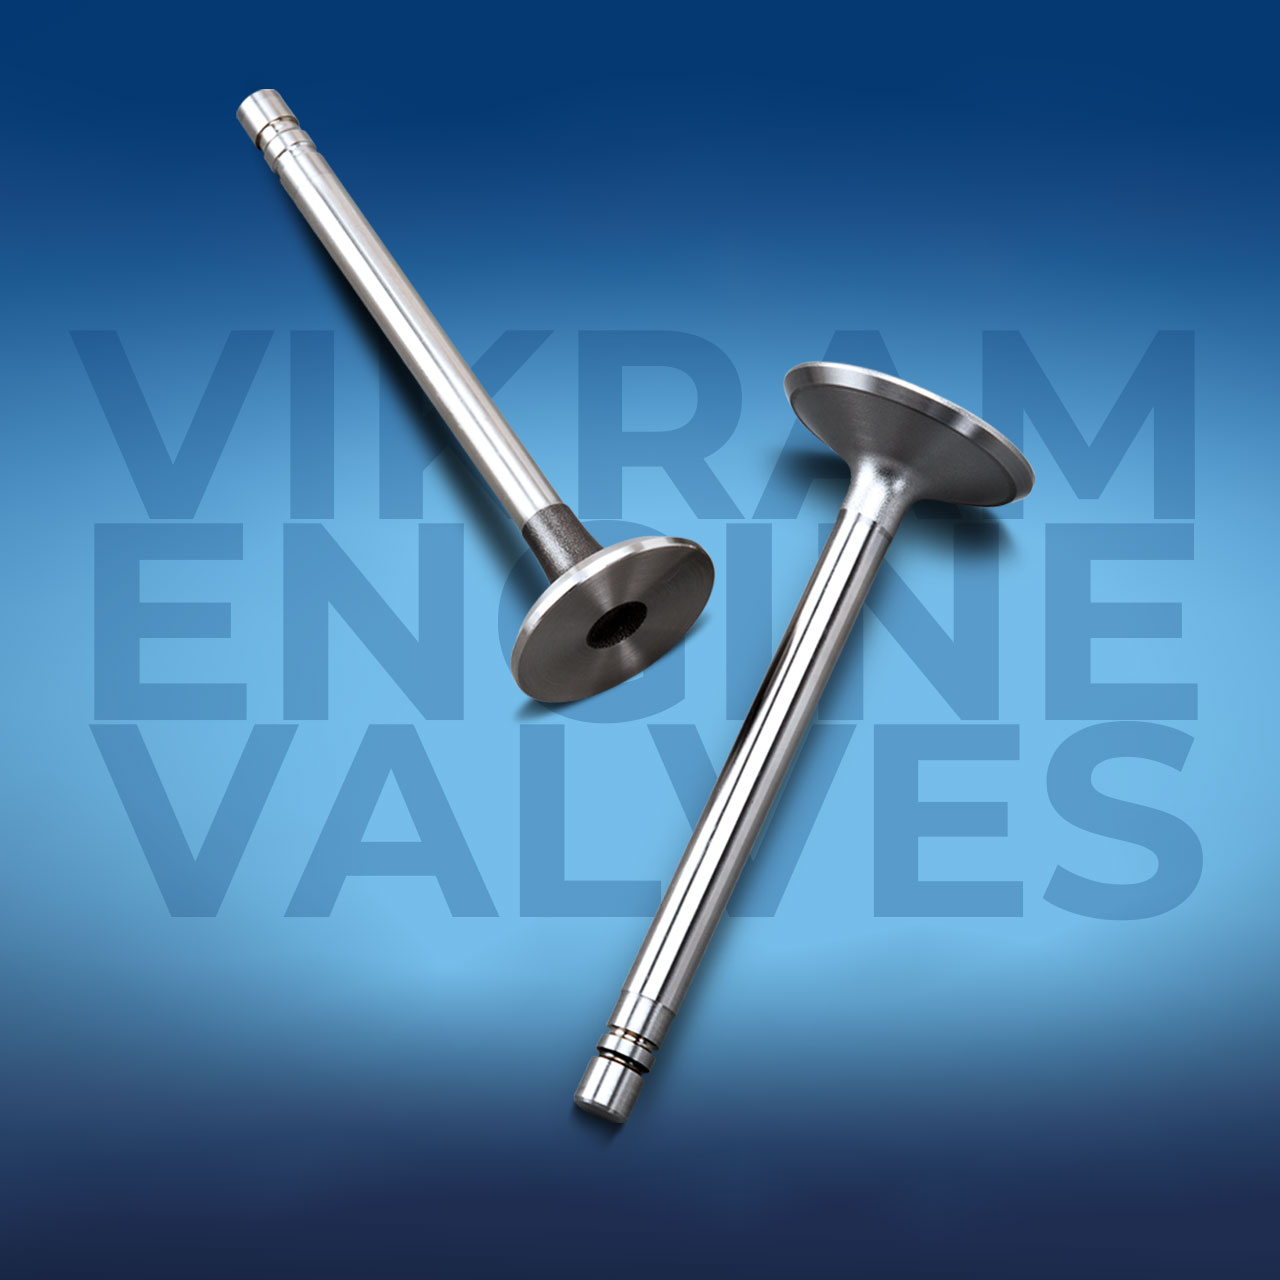
Engine valves operate at the heart of engine performance, controlling airflow, combustion efficiency, and thermal balance under extreme operating conditions. Designed to function reliably under high temperatures, cyclic loads, and continuous motion, they play a critical role in determining engine durability and output. Vikram engine valves are engineered with this responsibility in mind, delivering consistent sealing, accurate timing, and long service life across demanding applications.
Both intake and exhaust valves are manufactured using carefully selected materials and controlled processes to withstand heat, pressure, and wear. Material selection, heat treatment, and surface finishing are aligned with specific engine requirements, ensuring optimal resistance to fatigue, corrosion, and deformation. This engineering-led approach allows each valve to perform reliably throughout extended operating cycles.
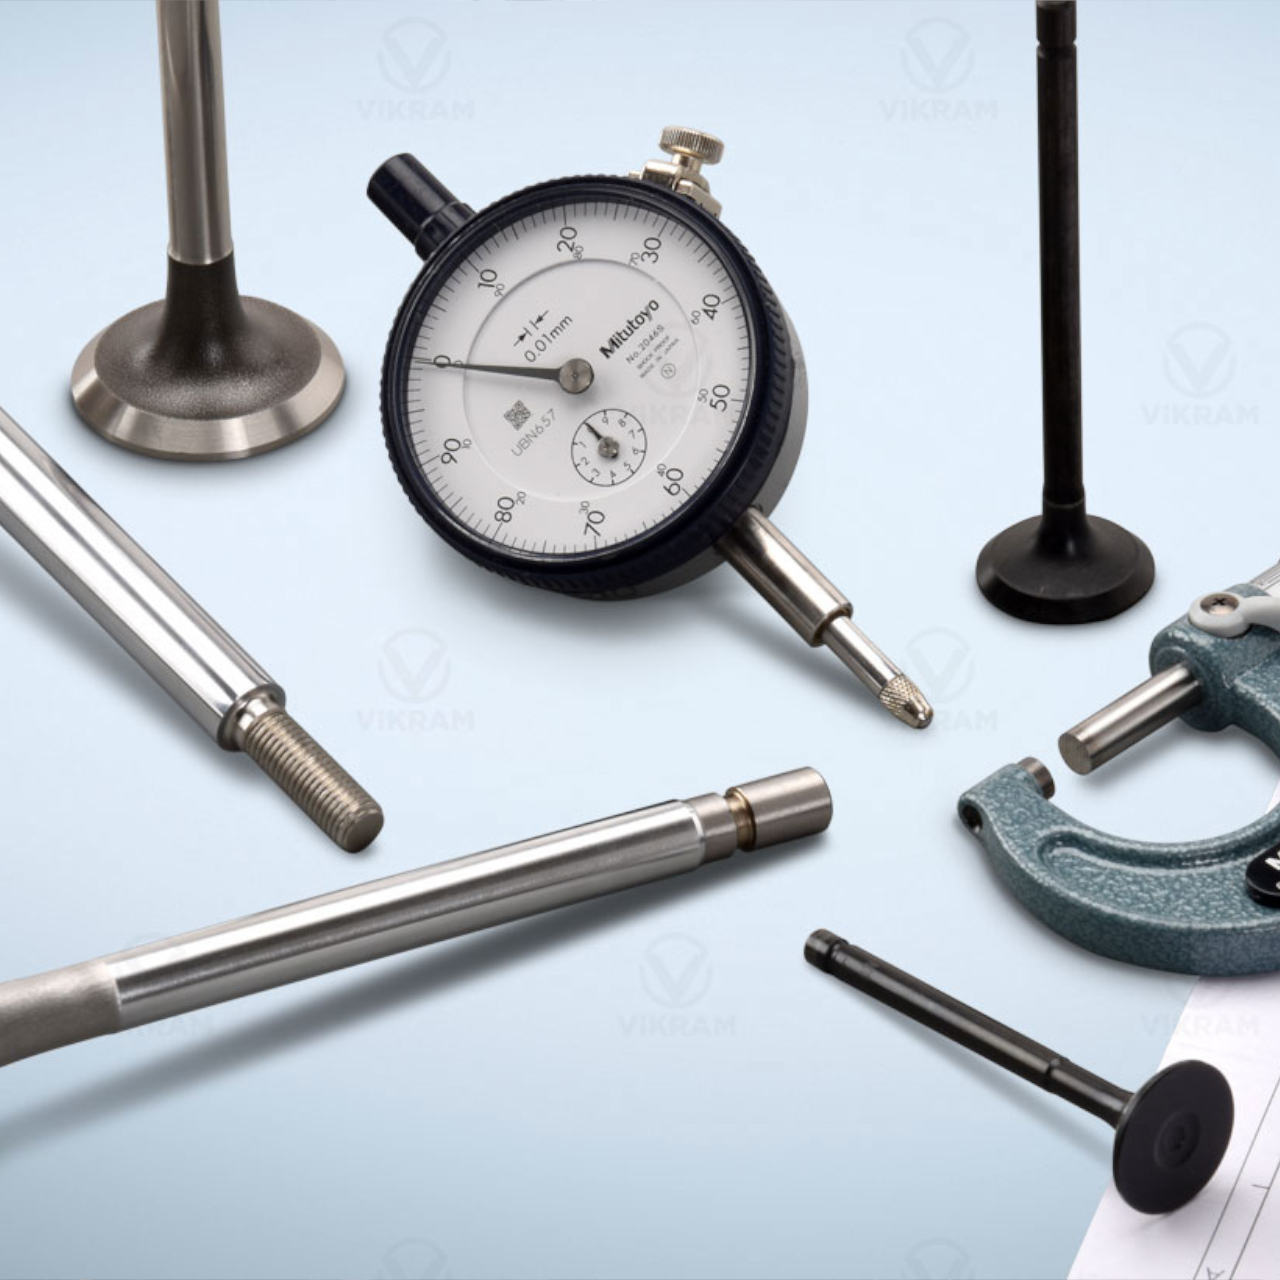
Manufacturing precision is supported by advanced manufacturing capabilities and rigorous in-process controls. From forging and machining to heat treatment and finishing, every stage is governed by defined parameters to maintain dimensional accuracy and metallurgical integrity. This consistency enables AVR (Vikram) Valves to supply engine valves that meet OEM specifications while delivering dependable performance in aftermarket applications.
With decades of experience in engine valve manufacturing for OEMs, AVR (Vikram) supports a wide range of engine platforms and duty cycles. Whether supplied for original equipment programs or replacement markets, each engine valve reflects the same focus on engineering discipline, material integrity, and controlled execution, ensuring performance that holds up in real-world operating environments.
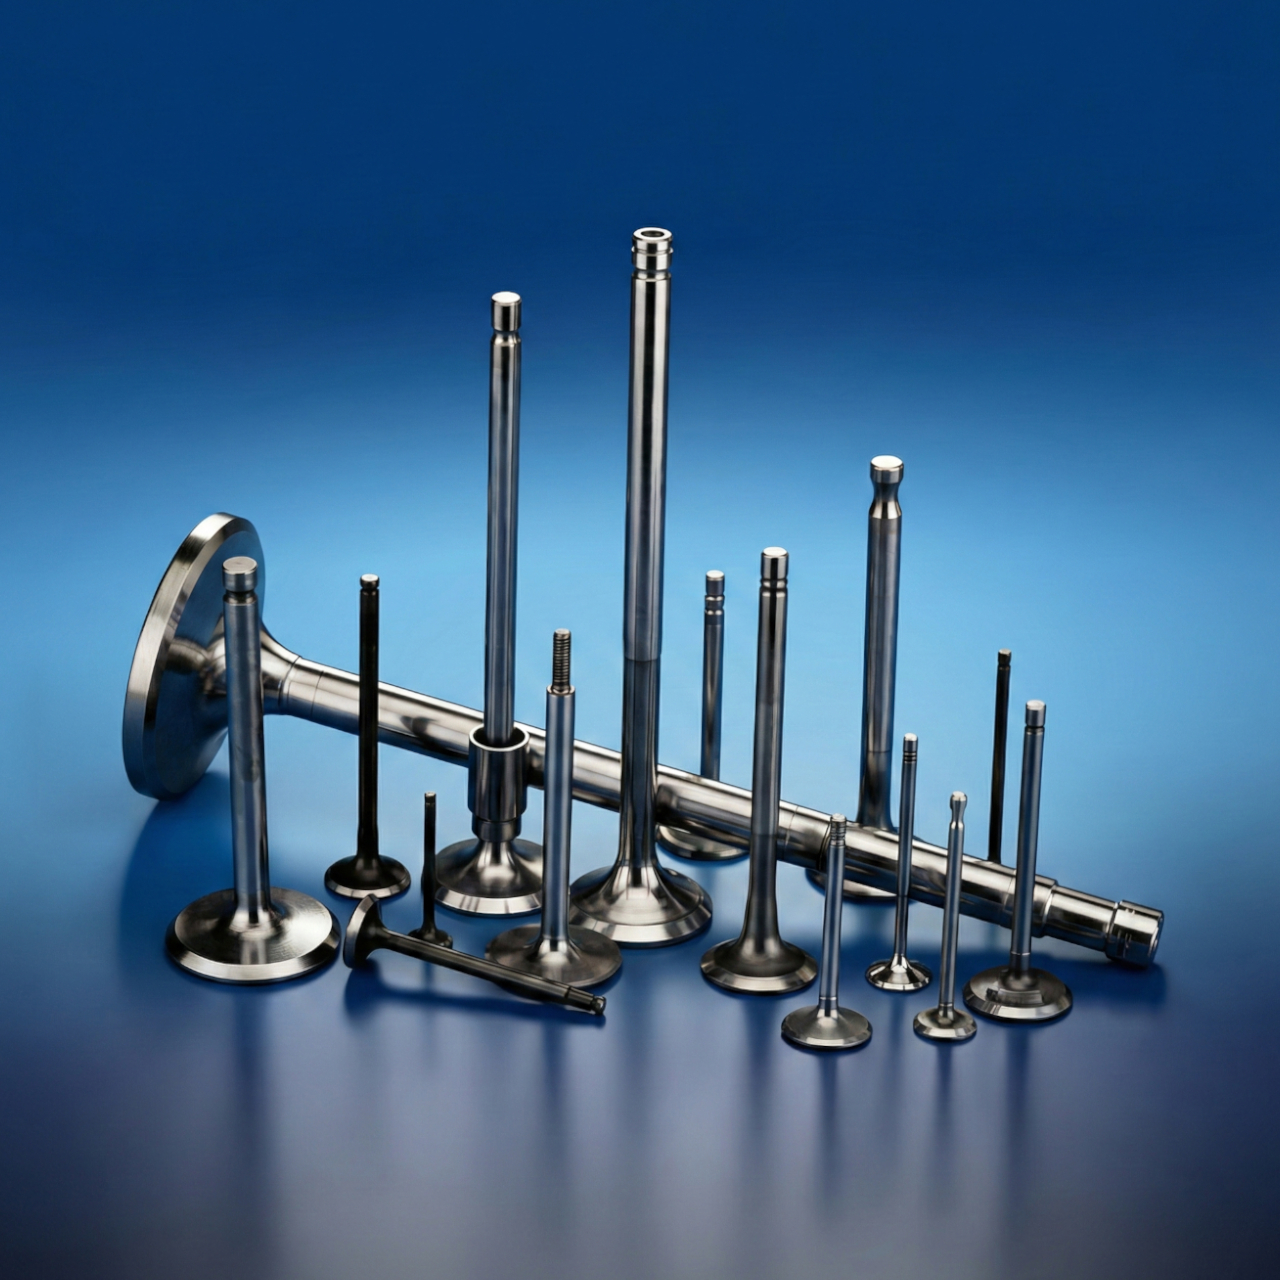
A broad engine valve manufacturing range, engineered processes, and application-driven design enable AVR (Vikram) Valves to support OEM and aftermarket engine programs at scale.
AVR (Vikram) Valves is a leading engine valve manufacturer in India, capable of producing more than 3,500 types of intake and exhaust engine valves for diverse automotive and industrial applications. This breadth lets us support a wide range of engine platforms, from high-volume passenger vehicles to heavy-duty, off-highway, and stationary engines.
Our manufacturing range covers valve stem diameters from 4 mm to 25 mm and valve lengths from 50 mm to 300 mm, enabling precise alignment with engine design requirements. Each valve is developed to meet defined performance parameters, ensuring accurate fitment, reliable sealing, and long service life under demanding operating conditions.
We manufacture engine valves for OEM programs, aftermarket applications, and custom requirements, applying the same engineering discipline and process control across all segments. Whether supplied as original equipment components, Vikram-branded aftermarket parts, or private-label solutions, every valve is produced to consistent quality standards.
Material selection and surface treatments are matched to performance demands. Depending on application requirements, engine valves are induction hardened, chrome plated, or nitrided, enhancing wear resistance, thermal stability, and service life. To protect reliability at scale, all critical characteristics are subjected to 100% inspection and crack detection, reinforcing confidence in every valve delivered.
Advanced materials, controlled manufacturing processes, and application-specific treatments are applied to enhance durability, efficiency, and long-term engine reliability.
A broad specification envelope enables precise matching across engine platforms, duty cycles, and performance requirements.
| SAE | BS | JS | Wr. No. | C | Si | Mn | Ni | Cr | Mo | N | |
|---|---|---|---|---|---|---|---|---|---|---|---|
| INTAKE & LIGHT DUTY EXHAUST | SIL1 | EN 52 | SUH 1 | 1,4718 | 0.40-0.50 | 3.00-3.50 | 0.60-MAX | 0.60-MAX | 7.50-9.50 | — | — |
| — | — | SUH 3 | — | 0.35-0.45 | 1.80-2.50 | 0.60-MAX | 0.60-MAX | 10.00-12.00 | 0.70-1.30 | — | |
| — | — | SUH 11 | — | 0.45-0.55 | 1.00-2.00 | 0.60-MAX | 0.60-MAX | 7.50-9.50 | — | — | |
| EXHAUST | EV-12 | 12-2 N | — | 14,875 | 0.50-0.60 | 0.08-0.25 | 7.00-9.50 | 1.50-2.75 | 19.25-21.50 | — | 0.20-0.40 |
| EV-8 | 21-4 N | SUH 35 | 14,871 | 0.48-0.58 | 0.35 MAX | 8.00-10.00 | 3.25-4.50 | 20.0-22.50 | — | 0.35-0.50 | |
| EV-15 | 23-8 N | — | — | 0.28-0.38 | 0.50-1.00 | 1.50-3.50 | 7.00-9.50 | 22.00-24.00 | — | 0.25-0.40 | |
| EV-4 | 21-12 N | SUH 37 | — | 0.15-0.25 | 1.00 MAX | 1.00-1.60 | 10.00-12.00 | 20.50-22.50 | — | 0.15-0.35 | |
| INCONEL-751 | 0.10 MAX | 0.50 MAX | 1.00 MAX | BAL | 14.0-17.0 | Ti/AL 2.2/1.0 | FE 7.0 | ||||
| NIMONIC-80A | 0.10 MAX | 1.00 MAX | 1.00 MAX | BAL | 18.0-21.0 | Ti/AL 2.0/1.5 | FE/CO 5.0/2.0 MAX MAX | ||||
| C | CR | W | FE | CO | |||
|---|---|---|---|---|---|---|---|
| STELLITE #1 | 2.5 | 30.0 | 12.0 | 3.0 MAX | BAL | HRC- | 50/54 |
| STELLITE #6 | 1.00 | 28.0 | 4.0 | 3.0 MAX | BAL | HRC- | 40/44 |
| STELLITE #12 | 1.35 | 29.0 | 8.0 | 2.0 MAX | BAL | HRC- | 45/47 |
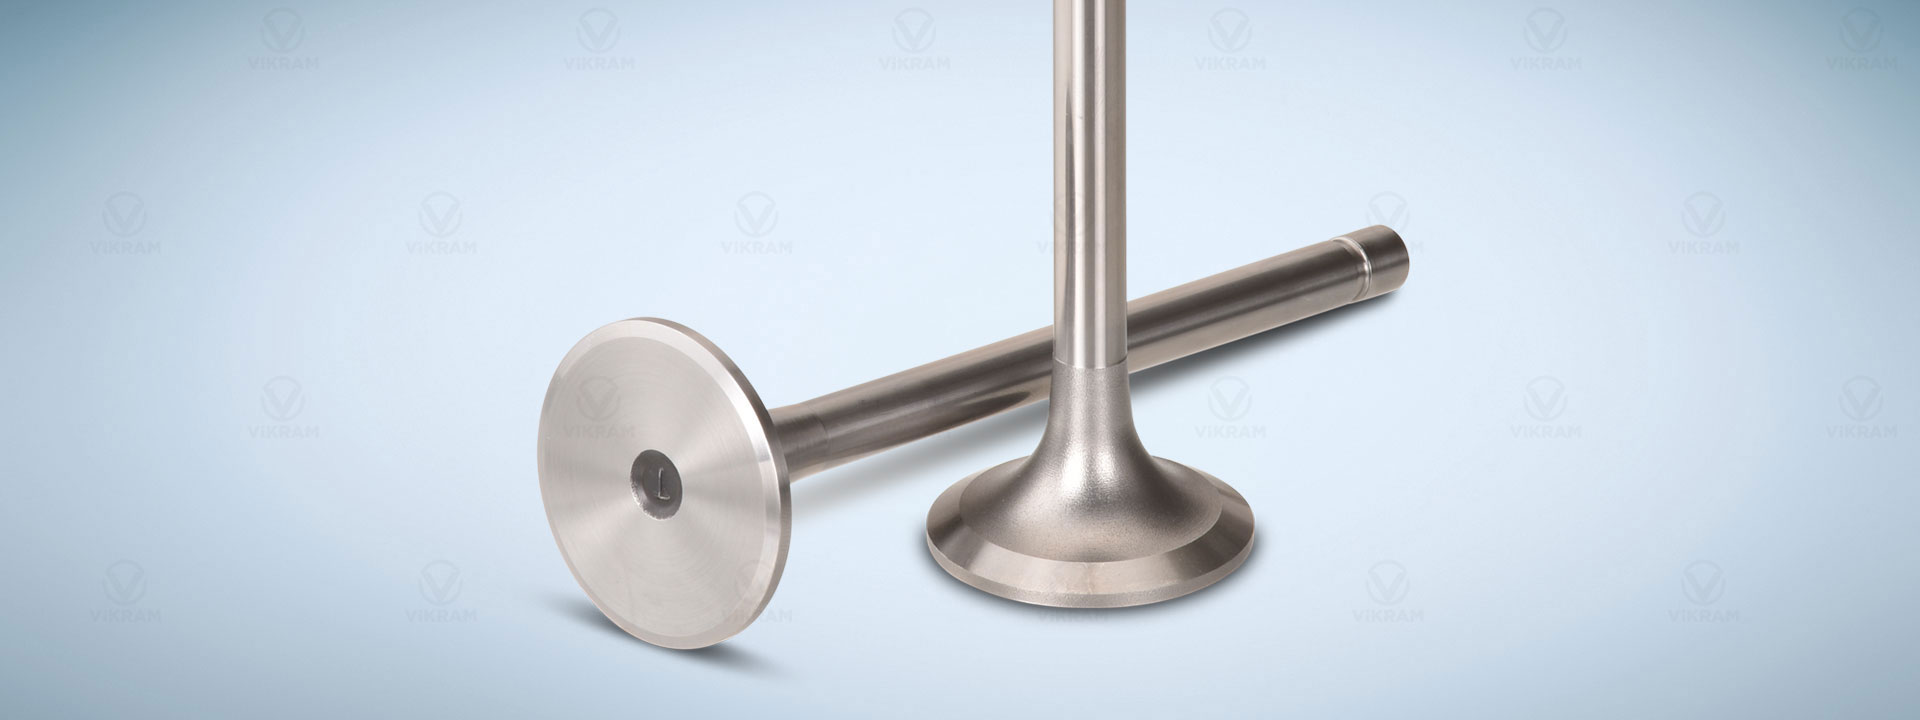
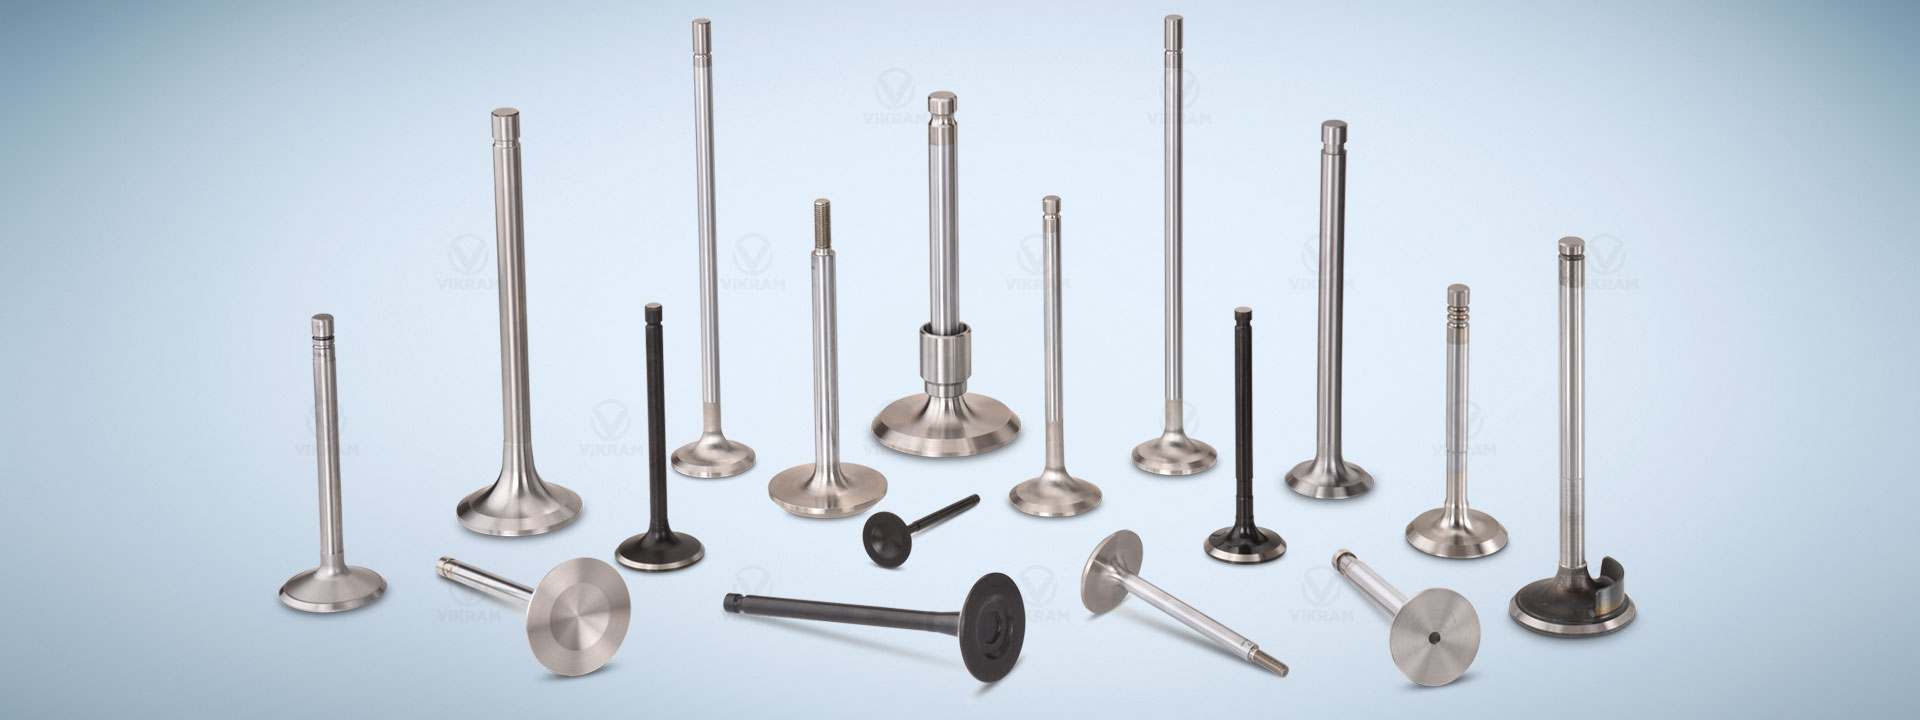
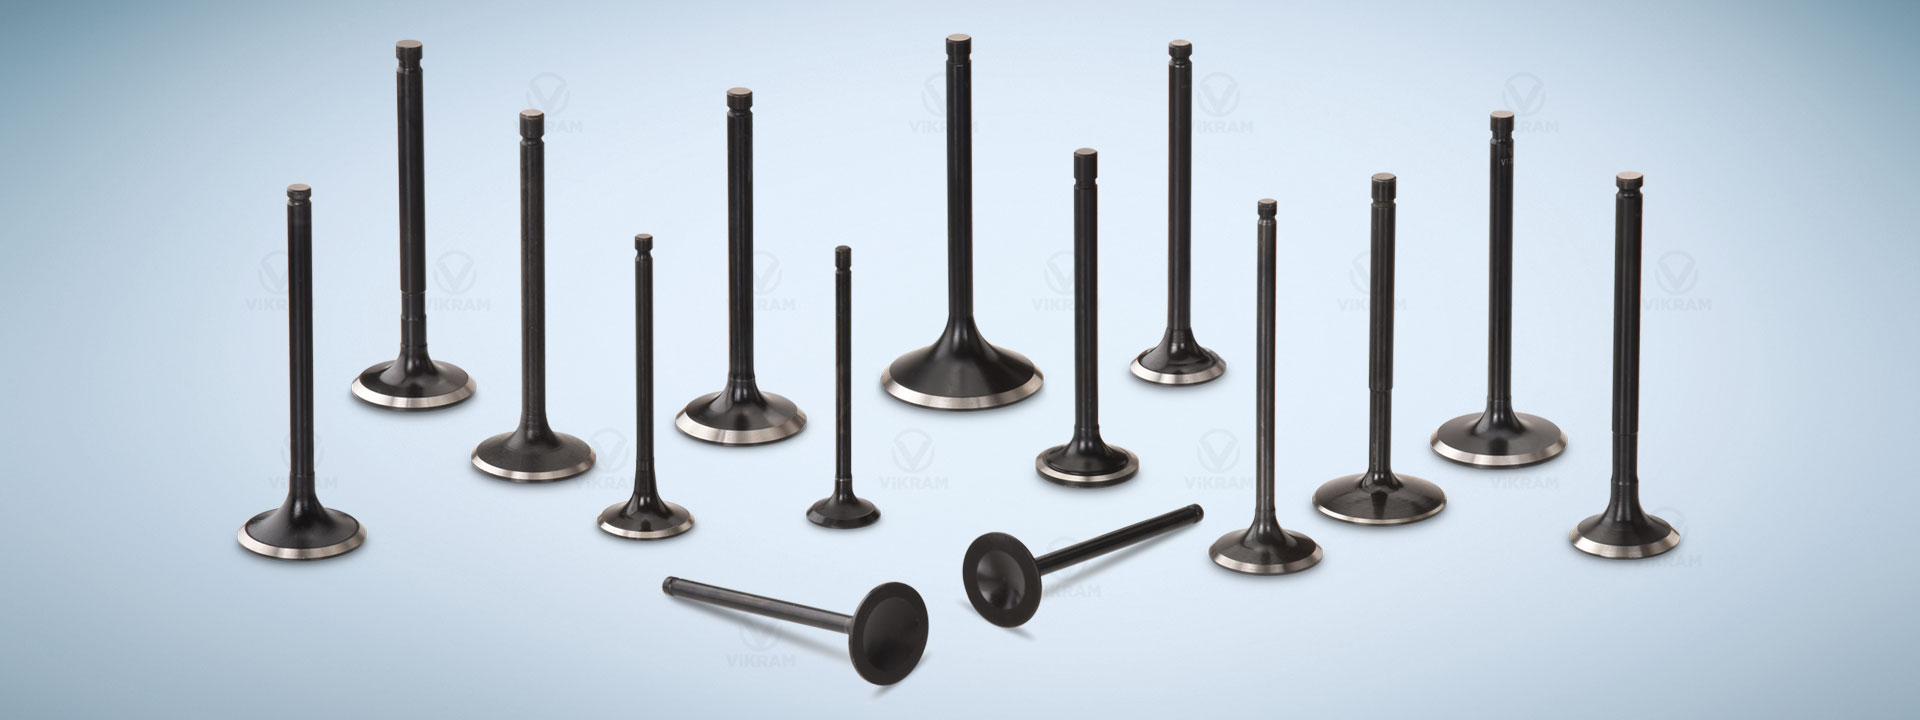
From design modification to full development, custom engine valves are built to match performance, durability, and operating conditions.
Standard engine valves don’t always meet the performance demands of specialized engines or evolving operating conditions. Custom engine valve development begins with a clear understanding of application requirements, duty cycles, material behavior, and interface constraints.
AVR (Vikram) Valves supports OEM and aftermarket customers with custom engine valve solutions from dimensional modifications and material upgrades to complete design development for new engine platforms. Engineering teams work closely with customer specifications to ensure design intent is translated into stable, repeatable production.
Material selection, heat treatment, surface coatings, and dimensional tolerances are optimized for operating temperature, load conditions, and service-life expectations. This disciplined approach ensures custom valves deliver consistent performance without compromising manufacturability or quality control.
Our in-house manufacturing, inspection, and validation capabilities support custom engine valve programs, enabling rapid development cycles while maintaining OEM-level quality standards.
Driving power across all segments.